

Industrial Dehumidifiers
Uncontrolled humidity causes product spoilage, corrosion, mould growth, condensation on machinery, and failed quality inspections. Sangawar Pneumatics manufactures industrial dehumidifiers using patented heatless technology that delivers over 50% energy savings compared to conventional systems — with a World Patent application filed. From pharmaceutical cleanrooms requiring 15% RH to large food processing halls needing stable atmospheric conditions, our dehumidifiers are custom-designed for your space, capacity, and humidity target. Manufactured at our Vasai facility and installed across India.
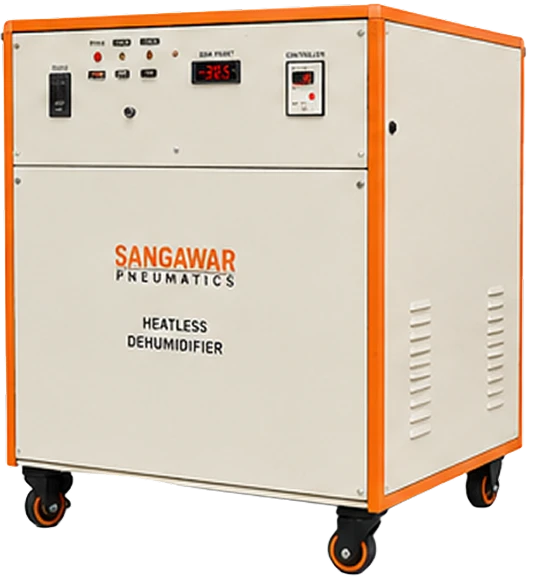
Heatless Dehumidifier (Patented Technology)
India's most energy-efficient industrial dehumidifier — using patented heatless adsorption technology to remove moisture from large industrial spaces without the energy penalty of conventional heating-based systems. Delivers over 50% energy savings in operation.
Features:
- Patented heatless operation — World Patent application filed
- Over 50% energy saving compared to conventional dehumidifiers
- Continuous drying with automatic desiccant regeneration cycle
Advantages:
- Dramatically lower electricity bills — measurable from day one
- No temperature rise in the treated space during operation
- Reliable, low-maintenance performance across seasons
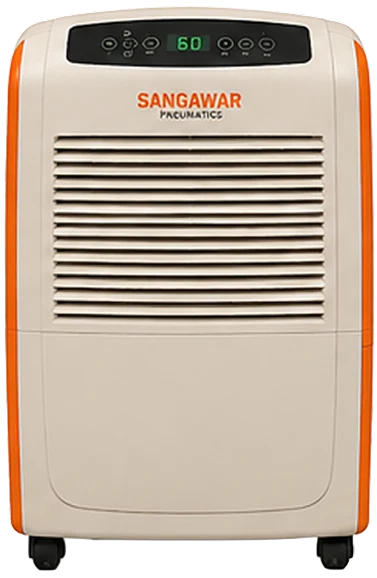
Refrigerated Industrial Dehumidifier
Robust industrial dehumidifier using cooling-based condensation to remove moisture from large spaces — designed and sized to your specific capacity and application requirements.
Features:
- Cooling coil condensation system for high-volume moisture removal
- Automatic drainage — no manual intervention required
- Compact, portable unit design for flexible deployment
Advantages:
- Straightforward operation with minimal training required
- Affordable solution for general industrial and commercial use
- Low maintenance with long operational service life
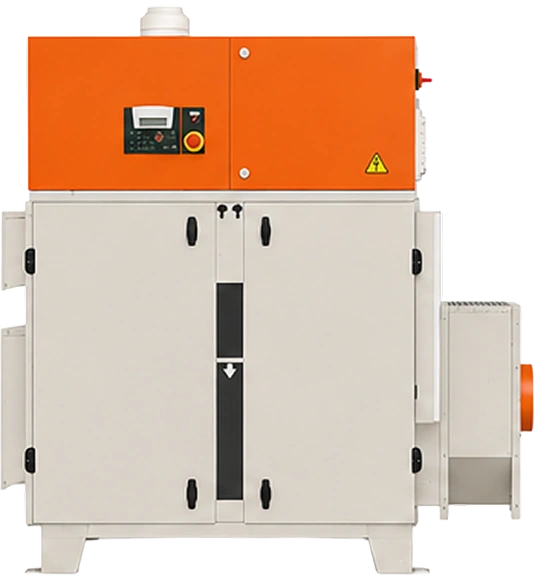
Low RH (15%) Dehumidifier
High-performance dehumidifier engineered to maintain extremely low relative humidity levels down to 15% RH — essential for pharmaceutical dry rooms, battery manufacturing, electronics assembly, and precision instrumentation storage.
Features:
- Maintains relative humidity as low as 15% RH
- Precision humidity sensor and automatic control system
- Robust construction for continuous cleanroom operation
Advantages:
- Meets stringent GMP and cleanroom humidity requirements
- Maintains stable environment regardless of ambient conditions
- High efficiency with low energy consumption per kg of moisture removed